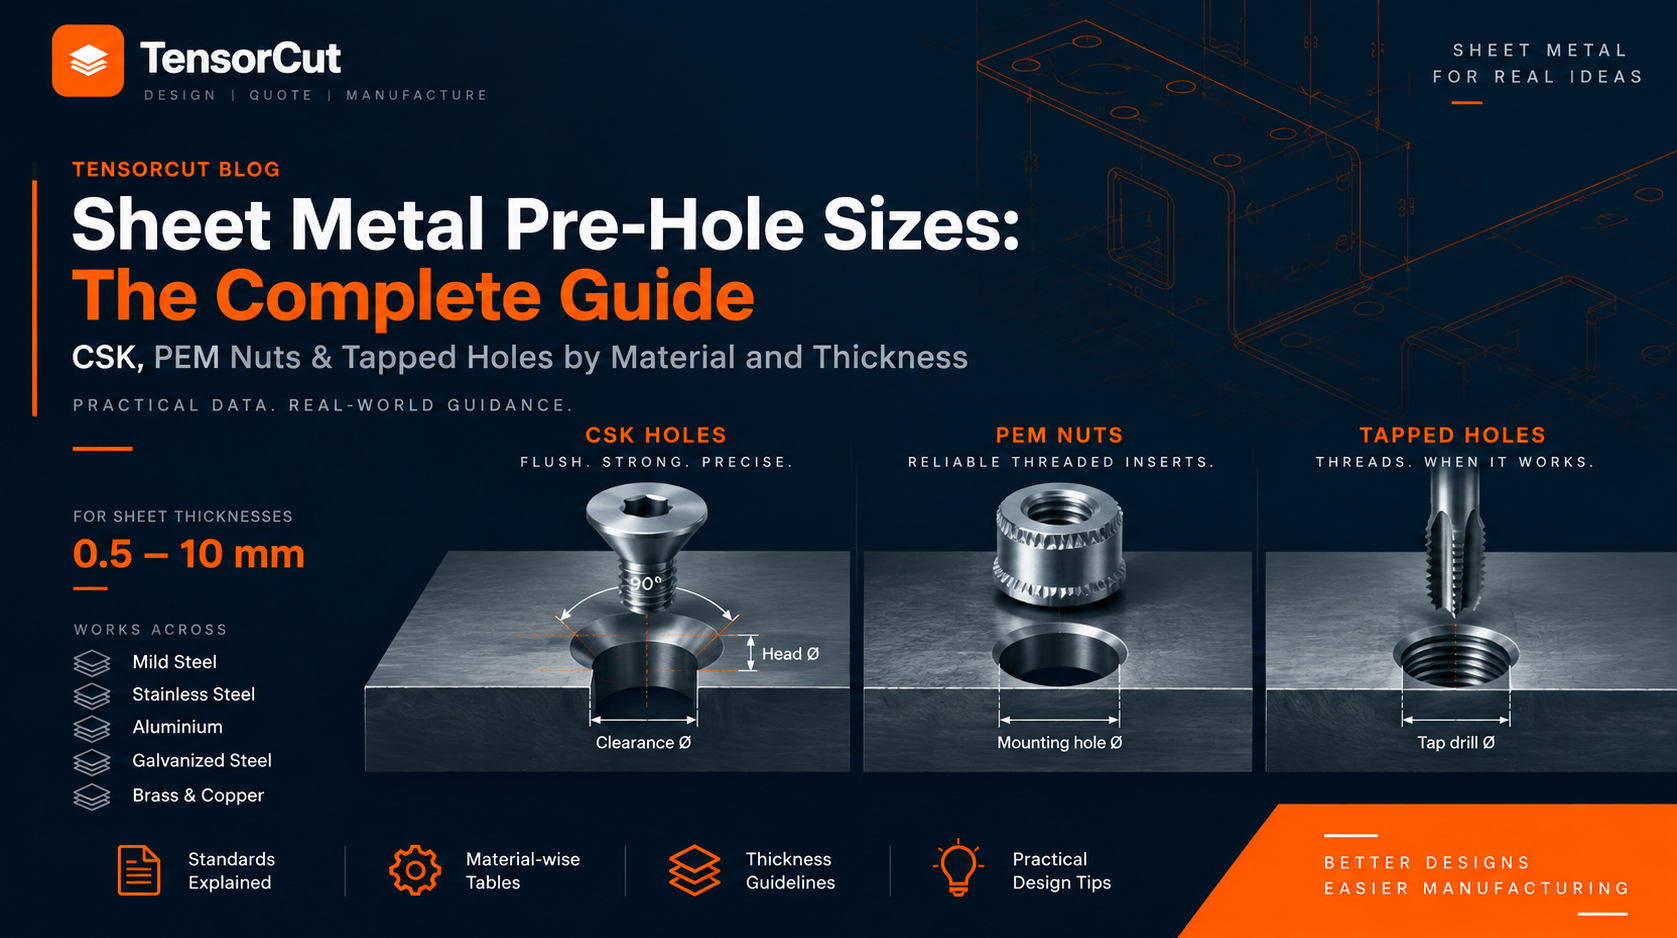
A practical guide to sheet-metal pre-hole sizes for CSK screws, PEM nuts, and tapped holes. Explore metric hole-size charts, material and thickness considerations, standards, and practical design guidelines for manufacturable parts.
Sheet Metal Pre-Hole Sizes: CSK, PEM Nuts & Tapped Holes by Material and Thickness
Designing a sheet-metal part is not just about drawing the final hole diameter. When a hole will be countersunk, tapped, or fitted with a PEM self-clinching nut, the hole in the flat sheet becomes a critical manufacturing feature.
A hole that is too small can cause assembly problems, excessive forming forces, or damaged fasteners. A hole that is too large can reduce thread engagement, cause a PEM nut to spin or pull out, or produce an unacceptable countersink.
This guide provides a practical engineering reference for designing pre-holes for countersunk screws (CSK), PEM self-clinching nuts, and tapped holes in sheet metal from approximately 0.5 mm to 10 mm thickness.
1. What Is a Pre-Hole?
A pre-hole is the hole created in the sheet before a secondary operation is performed. The secondary operation may be:
- countersinking for a CSK screw;
- installing a self-clinching PEM nut;
- tapping an internal thread;
- installing another type of insert or threaded hardware.
The important distinction is between the nominal feature and the manufacturing operation.
| Feature | Hole before secondary operation | Secondary operation | Final purpose |
|---|---|---|---|
| CSK screw | Clearance/pilot hole | Countersinking | Flush screw head |
| PEM nut | Specified mounting hole | Press installation | Permanent load-bearing internal thread |
| Tapped hole | Tap-drill hole | Tapping | Internal metric thread |
2. The Three Hole Types You Should Not Confuse
3. Metric Clearance Holes for CSK Screws
For a countersunk screw passing through a sheet, the first dimension to establish is the clearance hole. ISO 273 specifies general-purpose clearance-hole diameters in fine, medium and coarse series. For normal everyday assemblies, the medium/normal clearance series is a useful starting point.
| Metric screw | Pitch | Close clearance | Normal clearance | Loose clearance |
|---|---|---|---|---|
| M3 | 0.50 | 3.2 | 3.4 | 3.6 |
| M4 | 0.70 | 4.3 | 4.5 | 4.8 |
| M5 | 0.80 | 5.3 | 5.5 | 5.8 |
| M6 | 1.00 | 6.4 | 6.6 | 7.0 |
| M8 | 1.25 | 8.4 | 9.0 | 10.0 |
| M10 | 1.50 | 10.5 | 11.0 | 12.0 |
| M12 | 1.75 | 13.0 | 13.5 | 14.5 |
| M16 | 2.00 | 17.0 | 17.5 | 18.5 |
These dimensions are clearance-hole dimensions, not countersink diameters. The countersink must additionally accommodate the head geometry of the selected screw.
4. CSK Hole Design
A countersunk hole consists of two features:
- a through clearance hole; and
- a conical recess for the screw head.
For the common ISO 10642 hexagon socket countersunk screw, the nominal head diameter and head height increase with screw size. A 90° countersink is used.
| Screw | Pitch | ISO 10642 head diameter, nominal/max | Head height, max | Typical normal clearance hole |
|---|---|---|---|---|
| M3 | 0.50 | 6.72 mm | 1.86 mm | 3.4 mm |
| M4 | 0.70 | 8.96 mm | 2.48 mm | 4.5 mm |
| M5 | 0.80 | 11.20 mm | 3.10 mm | 5.5 mm |
| M6 | 1.00 | 13.44 mm | 3.72 mm | 6.6 mm |
| M8 | 1.25 | 17.92 mm | 4.96 mm | 9.0 mm |
| M10 | 1.50 | 22.40 mm | 6.20 mm | 11.0 mm |
4.1 How sheet thickness changes the CSK decision
The clearance diameter does not normally change just because the sheet becomes thicker. What changes is whether the sheet has enough material thickness to form the required countersink while retaining adequate material around the hole.
| Sheet thickness | CSK design consideration |
|---|---|
| 0.5–0.8 mm | Deep countersinks can remove a large percentage of the sheet thickness. Verify remaining wall thickness and consider a formed/dimpled countersink. |
| 1.0–1.5 mm | Small CSK screws may be practical, but large M6/M8/M10 countersinks require careful verification. |
| 2.0–3.0 mm | Conventional machining/countersinking becomes more practical for small and medium screw sizes. |
| 4.0–6.0 mm | Most common metric CSK sizes can generally be accommodated, subject to design requirements. |
| 8.0–10.0 mm | Countersinking is usually straightforward, but excessive countersink depth should still be avoided. |
For very thin sheet, a formed countersink, coined feature, embossment or other locally formed geometry may provide a better solution than simply removing material. The appropriate process depends on the required flushness, strength and production volume.
5. PEM Self-Clinching Nuts
PEM nuts solve a fundamental sheet-metal problem: a thin sheet may not contain enough material thickness to support a useful internal thread.
A self-clinching nut is installed into a prepared mounting hole. During installation, the sheet material flows around the nut's clinching feature and mechanically locks the fastener in place.
The critical point is that the mounting hole is not selected merely from the metric thread size.
For example, PennEngineering lists a mounting hole of 4.22 mm for several M3 self-clinching nut families, 5.41 mm for M4, 6.35 mm for M5, 8.75 mm for M6, 10.5 mm for M8 and 14 mm for M10 in its relevant S/CLS/SP metric families. The exact part number, shank code, sheet thickness and material hardness must still be checked before manufacture.
5.1 PEM mounting-hole reference
| Thread | Pitch | Typical PEM mounting hole* | Representative minimum sheet thickness* |
|---|---|---|---|
| M2 | 0.40 | 4.22 mm | 0.8 mm |
| M2.5 | 0.45 | 4.22 mm | ~0.8–1.4 mm depending on shank |
| M3 | 0.50 | 4.22 mm | ~0.8–1.0 mm depending on shank |
| M4 | 0.70 | 5.41 mm | ~0.8–1.4 mm depending on shank |
| M5 | 0.80 | 6.35 mm | ~0.8–1.4 mm depending on shank |
| M6 | 1.00 | 8.75 mm | ~1.2 mm and above depending on shank |
| M8 | 1.25 | 10.50 mm | ~1.4 mm and above depending on shank |
| M10 | 1.50 | 14.00 mm | ~2.3 mm and above depending on shank |
*Important: These are representative values from PEM's metric self-clinching nut families, not a substitute for selecting a specific PEM part. For production drawings, use the mounting-hole specification for the exact fastener part number.
5.2 PEM nuts by material
| Sheet material | Typical PEM family consideration | Important requirement |
|---|---|---|
| Carbon / mild steel | S / CLS families | Check material hardness and exact fastener specification. |
| Aluminium | S / CLS families are commonly available | Check sheet hardness and minimum thickness; soft aluminium may require a suitable fastener family. |
| Stainless steel | SP / stainless-sheet-specific families | Use a fastener specifically approved for stainless sheet. Do not assume a standard steel-sheet PEM nut is interchangeable. |
| Galvanized steel | Depends on coating and substrate | Consider coating thickness, hardness and installation method. |
PennEngineering specifies different material-hardness limits for different families. For example, Type SP is intended for stainless-steel sheets within specified hardness limits, while S/SS and CLS/CLSS families have their own steel/aluminium hardness limits. This is why "M6 PEM nut" is not a sufficiently complete manufacturing specification.
5.3 PEM installation: what designers need to know
The mounting hole should be manufactured to the fastener manufacturer's specified diameter. The hole should not be treated like an ordinary clearance hole.
PEM's installation guidance calls for a properly sized mounting hole and specifically warns against deburring the mounting hole before installation because deburring removes material needed for the clinching action. The fastener should be installed with appropriate squeezing force and parallel punch/anvil surfaces rather than hammered into the sheet.
6. Tapped Holes in Sheet Metal
A tapped hole is different from a PEM hole. Instead of inserting a separate threaded component, the internal thread is formed directly in the sheet.
The pre-hole for a standard metric cutting tap is commonly selected from the tap manufacturer's recommended drill-size table. The exact hole diameter is influenced by the desired percentage of thread, thread tolerance, material, tap geometry and application.
6.1 Common metric coarse-thread tap-drill sizes
| Thread | Pitch | Common tap drill | Nominal thread depth required for direct sheet tapping |
|---|---|---|---|
| M3 × 0.5 | 0.50 | 2.5 mm | Application dependent |
| M4 × 0.7 | 0.70 | 3.3 mm | Application dependent |
| M5 × 0.8 | 0.80 | 4.2 mm | Application dependent |
| M6 × 1.0 | 1.00 | 5.0 mm | Application dependent |
| M8 × 1.25 | 1.25 | 6.8 mm | Application dependent |
| M10 × 1.5 | 1.50 | 8.5 mm | Application dependent |
| M12 × 1.75 | 1.75 | 10.2 mm | Application dependent |
These values are common starting points for ISO coarse threads and are consistent with published tap-manufacturer data. For production work, the tap manufacturer and required thread percentage should control the final drill size.
7. Why Sheet Thickness Matters for Tapped Holes
The tap-drill diameter itself does not normally change simply because a sheet is 0.8 mm instead of 2 mm thick. What changes dramatically is the amount of usable thread engagement.
For a directly tapped sheet, the designer needs enough fully formed thread to carry the intended load. As a practical engineering rule, approximately 1 × nominal diameter of engagement in steel and approximately 2 × nominal diameter in aluminium are commonly used starting points, but the exact required engagement depends on bolt grade, parent material, thread class, load case and safety factor.
| Sheet thickness | Direct tapping guidance |
|---|---|
| 0.5–0.8 mm | Direct conventional tapping is generally unsuitable for many standard metric sizes because available thread engagement is very small. Consider a PEM nut, formed/extruded thread, or other insert. |
| 1.0–1.5 mm | Small threads may be possible for lightly loaded applications, but available engagement must be checked carefully. |
| 2.0–3.0 mm | M3/M4/M5 and some larger threads may be practical depending on material and load. |
| 4.0–6.0 mm | Direct tapping becomes substantially more practical for common metric sizes. |
| 8.0–10.0 mm | Many common metric threads can obtain substantial engagement, subject to design loads and material. |
8. Material-Specific Tapping Considerations
Carbon / Mild Steel
Mild steel is generally well suited to conventional tapping when adequate thickness and thread engagement are available. Cutting conditions, lubrication, tap geometry and hole quality affect tool life and thread quality.
For thin sheet, a PEM nut or formed thread can provide more useful engagement than attempting to obtain a full thread directly in the sheet.
Stainless Steel
Stainless steels require more attention to work hardening, lubrication and tap selection. A poorly controlled tapping operation can increase tool wear and create dimensional problems.
For very thin stainless sheet, a self-clinching solution specifically designed for stainless material may be more appropriate than direct tapping.
Aluminium
Aluminium is relatively easy to tap, but its lower thread shear strength means that thread engagement can become the limiting factor. More engagement is often required than in steel for the same fastener load.
Where sheet thickness does not provide sufficient engagement, use a suitable insert, PEM nut, or formed-thread feature.
Galvanized Steel
Galvanized sheet requires consideration of the coating as well as the underlying steel. Secondary operations may expose bare steel, affect corrosion protection, or create coating debris.
Brass and Copper
Brass and copper are generally machinable, but their strength varies substantially by alloy and temper. Do not use a single engagement multiplier for every copper or brass alloy. Check the material specification and joint loading.
9. CSK vs PEM vs Tapped Hole: Which Should You Use?
| Requirement | CSK | PEM nut | Direct tapping |
|---|---|---|---|
| Flush external screw head | Excellent | Possible with appropriate hardware | Not the primary purpose |
| Very thin sheet | Possible, but countersink depth is critical | Excellent | Often limited |
| High assembly torque | Depends on joint | Good when correctly selected | Depends on thread engagement |
| Replaceable internal thread | No | Yes | No |
| Low-cost single-piece construction | Yes | Requires hardware installation | Yes |
| Very thin aluminium | Possible | Often useful | Often requires more engagement |
10. Master Quick-Reference Table
| Feature | M3 | M4 | M5 | M6 | M8 | M10 |
|---|---|---|---|---|---|---|
| Normal CSK clearance | 3.4 | 4.5 | 5.5 | 6.6 | 9.0 | 11.0 |
| Typical PEM mounting hole* | 4.22 | 5.41 | 6.35 | 8.75 | 10.50 | 14.00 |
| Tap drill, coarse thread | 2.5 | 3.3 | 4.2 | 5.0 | 6.8 | 8.5 |
| Typical ISO 10642 CSK head Ø | 6.72 | 8.96 | 11.20 | 13.44 | 17.92 | 22.40 |
All dimensions are in millimetres.
*PEM values are representative mounting-hole values for relevant PEM metric families. Always verify the exact PEM part number before production.
11. Recommended Hole Rules for CAD Designers
- For a CSK screw: specify the screw standard, clearance hole and countersink angle/diameter. Do not rely on a generic "CSK" label.
- For a PEM nut: specify the exact PEM part number wherever possible. The thread size alone does not uniquely define the mounting hole.
- For a tapped hole: specify thread designation and tolerance, for example M6 × 1 - 6H, rather than simply "M6".
- For thin sheet: evaluate available thread engagement before choosing direct tapping.
- For aluminium: pay particular attention to thread stripping and engagement because the parent material may be substantially weaker than the screw.
- For stainless steel: select the tapping process and PEM family for the specific stainless grade and hardness.
- For PEM holes: avoid unnecessary deburring before fastener installation because the manufacturer's clinching mechanism relies on the sheet material around the mounting hole.
- For laser-cut, punched or machined holes: account for the actual manufacturing process and hole quality. The nominal CAD diameter is not always the same as the process's guaranteed finished diameter.
12. Laser Cutting, Punching, Drilling and Machining
Although these design rules apply to sheet-metal fabrication generally, the manufacturing process still matters.
| Process | Important consideration |
|---|---|
| Laser cutting | Kerf, taper, heat input, material thickness and process calibration can affect the finished hole. |
| Punching | Tool clearance, slug formation, work hardening and die condition affect hole quality. |
| Drilling | Usually gives good control for secondary operations but adds an additional manufacturing operation. |
| Machining | Can provide tighter dimensional control for precision holes and countersinks. |
For PEM installation in particular, the hole should be manufactured to the fastener manufacturer's specified mounting-hole size. PennEngineering's installation guidance emphasizes using the specified hole and avoiding pre-installation deburring.
13. Hole-to-Edge Distance
Hole diameter is only one part of good sheet-metal hole design. The distance between a hole and the sheet edge can be equally important.
For PEM fasteners, the manufacturer publishes a minimum hole-center-to-edge dimension for each fastener. This dimension should be treated as a controlled fastener requirement rather than replaced with a generic sheet-metal rule.
For ordinary clearance holes, keep sufficient material between the hole and edge to prevent deformation during assembly and service. The exact requirement depends on load, sheet thickness, hole size and joint configuration.
14. Common Design Mistakes
Mistake 1: Using the tap drill as the clearance hole
A 5.0 mm M6 tap drill is not an M6 clearance hole. An M6 clearance hole is substantially larger because the screw must pass freely through the sheet.
Mistake 2: Assuming every M5 PEM nut uses the same hole
Different PEM product families and configurations can have different installation requirements. Always verify the manufacturer's drawing.
Mistake 3: Countersinking without checking sheet thickness
A countersink that is geometrically correct can still remove too much material from thin sheet.
Mistake 4: Tapping a hole that is too shallow
The tap may produce a visually acceptable thread, but the joint may still have insufficient thread engagement for the required load.
Mistake 5: Deburring a PEM mounting hole
For self-clinching fasteners, removing material around the hole can interfere with the intended clinching mechanism. Follow the fastener manufacturer's installation procedure.
15. TensorCut Design Cheat Sheet
Need a countersunk screw?
Step 1: Identify the screw standard and size.
Step 2: Select the clearance hole from the appropriate standard.
Step 3: Specify the countersink angle and head diameter.
Step 4: Check that the countersink depth is compatible with the sheet thickness.
Need a PEM nut?
Step 1: Select the exact PEM fastener family and part number.
Step 2: Use the manufacturer's mounting-hole diameter.
Step 3: Check minimum sheet thickness and sheet hardness.
Step 4: Check minimum hole-center-to-edge distance.
Step 5: Install using controlled squeezing force and the specified tooling.
Need a tapped hole?
Step 1: Select the thread designation, e.g. M6 × 1 - 6H.
Step 2: Select the appropriate tap drill.
Step 3: Check available thread engagement.
Step 4: Check the material's strength and tapping characteristics.
Step 5: If the sheet is too thin, consider a PEM nut, insert or formed thread.
16. Frequently Asked Questions
What hole size should I use for an M5 countersunk screw?
For a normal clearance fit, an M5 screw commonly uses a 5.5 mm clearance hole. The countersink itself must then be sized to the selected screw head geometry. For an ISO 10642 socket countersunk screw, the nominal maximum head diameter is 11.2 mm.
What is the M6 tap drill size?
A common starting value for an M6 × 1.0 cutting tap is a 5.0 mm drill. The final process specification should be confirmed against the selected tap, thread percentage and material.
Can I tap a 1 mm sheet for M6?
It may be physically possible to form some thread, but the available thread engagement is only around the sheet thickness and is generally insufficient for many conventional M6 applications. A PEM nut, insert or formed-thread feature should be evaluated instead.
Does aluminium require a different tap drill diameter?
The nominal tap-drill selection is not simply changed because the material is aluminium. However, the desired thread percentage, tap geometry, cutting conditions and application can influence the recommended hole size. The tap manufacturer's data should control the production value.
Can I laser cut a PEM hole?
A laser can produce a nominal mounting hole, but the final suitability depends on the actual hole geometry, taper, dimensional capability and the PEM manufacturer's installation requirements. For production PEM applications, validate the actual process with the selected fastener and sheet material.
What is the difference between a PEM hole and a tap-drill hole?
A PEM mounting hole is designed to mechanically retain a separate fastener. A tap-drill hole is deliberately undersized so material remains around the hole for an internal thread to be cut.
17. Standards and Engineering References
- ISO 273 — Fasteners — Clearance holes for bolts and screws
- ISO 68-1:2023 — ISO general purpose screw threads — Basic and design profiles
- ISO 262:2023 — Selected metric sizes for bolts, screws, studs and nuts
- ISO 724:2023 — ISO general purpose metric screw threads — Basic dimensions
- ISO 965-1:2026 — Metric screw-thread tolerances — Principles and basic data
- ISO 965-2:2024 — Metric screw-thread tolerance limits
- ISO 10642 — Hexagon socket countersunk head screws
- PennEngineering PEM self-clinching nut installation specifications
18. Final Takeaway
The most important lesson is that there is no single universal "sheet-metal pre-hole chart".
CSK holes are governed by the screw's clearance requirement and head geometry.
PEM holes are governed by the exact self-clinching fastener, sheet thickness, sheet hardness and installation requirements.
Tapped holes are governed by the thread specification, tap-drill size, material and available thread engagement.
For a manufacturing platform such as TensorCut, these rules can eventually be turned into automated CAD design checks. Instead of simply telling a customer that a hole is "too small", a quoting engine can identify the feature and return a manufacturing recommendation such as:
M6 tapped hole detected in 1.2 mm aluminium sheet.
Available engagement: approximately 1.2 mm.
Recommendation: Consider PEM M6 fastener or formed-thread solution instead of direct conventional tapping.
That is the direction in which intelligent sheet-metal quoting can move: from simply manufacturing the geometry a customer uploads to actively helping the designer create geometry that is easier, stronger and more economical to manufacture.
Design it. Upload it. Manufacture it.
With TensorCut, turn your sheet-metal CAD into real manufactured parts without the usual back-and-forth.